Address
Building 1, No. 22, Shexi Yongping Road,
Dongguan, Guangdong, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
Building 1, No. 22, Shexi Yongping Road,
Dongguan, Guangdong, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Returnable packaging KPIs should cover trip count, return ratio, cycle time, loss rate, damage rate, washing cost and cost per ... Ask Mingskye for a sample.
Returnable packaging KPIs should cover trip count, return ratio, cycle time, loss rate, damage rate, washing cost and cost per trip, each measured per route rather than as a company-wide average. A single average hides the destination that is holding containers for three weeks. Review the set monthly for the first quarter, then quarterly. Record how each figure is calculated so the trend stays comparable.
This page covers returnable packaging KPIs in six sections: Static rating versus a working warehouse; Sequenced delivery to an assembly line; Terms that appear on a box drawing; Recycling route and take-back; Measured returns in the first quarter; Writing the end-of-life plan early. Each section answers one practical question and can be read on its own.
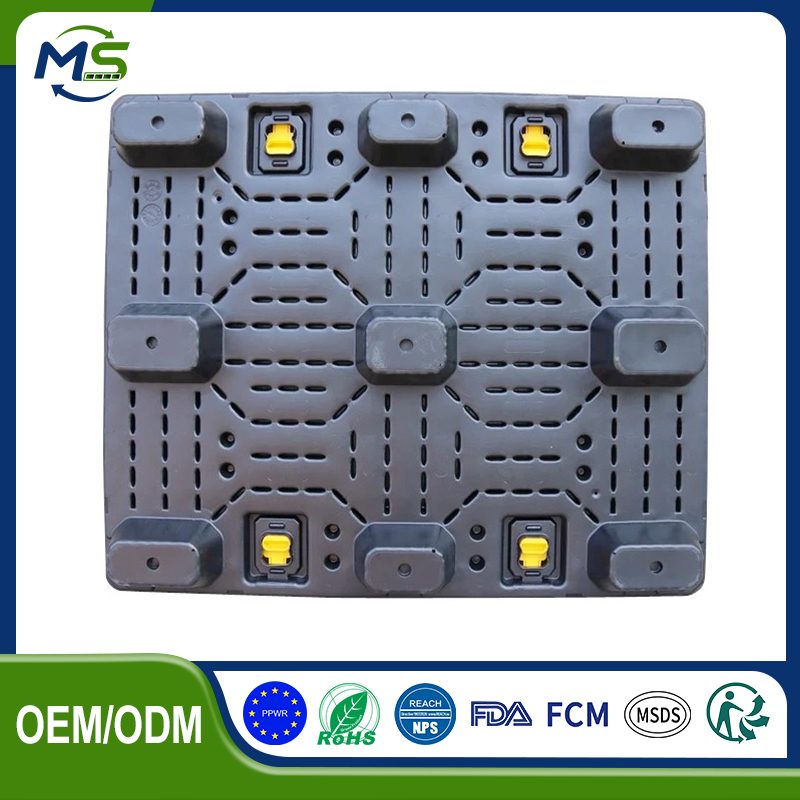
A static compression figure describes a controlled test, while a working warehouse adds braking, handling and time.
In the test the load is applied evenly, at a fixed temperature, for a stated duration. On the dock it arrives slightly off centre, sits through a warm weekend and is moved twice by a forklift before anyone checks it again.
Ask the supplier to describe the test conditions in one line. If the duration or the temperature is missing, the number cannot be reproduced and should not be used as a warehouse limit.
Sequencing asks a container to arrive with parts in build order, which makes consistency more valuable than maximum capacity.
The same outer footprint has to fit the line-side rack every time, and the empty has to leave on the vehicle that delivered it. A container that varies by a few millimetres between batches can disturb a rack pattern that was set months earlier.
Agree the labelling position with the assembly plant before tooling. A mark that is hidden once the box is on the rack is effectively absent to the operator working at the line.
For terminology and test-method context see GHG Protocol Corporate Value Chain (Scope 3) Accounting and Reporting Standard. The guidance on this page is practical handling guidance, not a test report or a certificate.
A drawing uses a small vocabulary that has to mean the same thing to the buyer, the toolmaker and the receiving dock.
Tare weight is the empty container with all its fittings. Internal clear dimension is the usable space after dividers and wall thickness. Fold height is the assembled height of an empty unit collapsed for return. Stack load is a figure that only means something with its test conditions attached.
Write the definitions into the enquiry rather than assuming a shared vocabulary. Two suppliers can both quote a stack load while measuring completely different durations and temperatures.
| Operations question | Short answer | Measure to track | In this guide |
|---|---|---|---|
| What should be checked about static rating versus a working warehouse? | A static compression figure describes a controlled test, while a working warehouse adds braking, handling and … | In the test the load is applied evenly, at a fixed temperature, for a stated … | Section 1 |
| What should be checked about sequenced delivery to an assembly line? | Sequencing asks a container to arrive with parts in build order, which makes consistency more valuable … | The same outer footprint has to fit the line-side rack every time, and the empty … | Section 2 |
| What should be checked about terms that appear on a box … | A drawing uses a small vocabulary that has to mean the same thing to the buyer … | Tare weight is the empty container with all its fittings. Internal clear dimension is the … | Section 3 |
| What should be checked about recycling route and take-back? | An end-of-life plan is only real when a named operator will accept the material. | Ask whether the supplier takes back rejected units, which local recycler handles the polymer, and … | Section 4 |
An end-of-life plan is only real when a named operator will accept the material.
Ask whether the supplier takes back rejected units, which local recycler handles the polymer, and what preparation is required before collection. Grinding a container with a hinge still attached may not be accepted.
Record the name, the accepted material and the collection frequency. If any of the three is unknown at the time of the first order, the plan is an intention rather than a route.
The first quarter of a pool produces the return ratio that every later calculation depends on.
Count containers dispatched and containers received back clean, week by week, at each destination. Resist adjusting the figures for exceptional weeks; the exceptions are exactly what the buffer has to absorb.
Review the trend with both site owners at the end of the quarter. A ratio that improves after a single conversation about the dispatch note is a process fix, not a product result.
The cheapest time to design an end-of-life route is before the first production order is signed.
At that point the material, the fittings, the ink and the markings are all still choices. Once a fleet is in service, changing any of them creates two specifications in the same pool.
Keep the plan with the drawing revision and the sample photographs. When the fleet is eventually replaced, that file explains what the containers were made of and where they were meant to go.
A static compression figure describes a controlled test, while a working warehouse adds braking, handling and time. In the test the load is applied evenly, at a fixed temperature, for a stated duration. On the dock it arrives slightly …
Sequencing asks a container to arrive with parts in build order, which makes consistency more valuable than maximum capacity. The same outer footprint has to fit the line-side rack every time, and the empty has to leave on the vehicle that …
An end-of-life plan is only real when a named operator will accept the material. Ask whether the supplier takes back rejected units, which local recycler handles the polymer, and what preparation is required before collection. Grinding …
The cheapest time to design an end-of-life route is before the first production order is signed. At that point the material, the fittings, the ink and the markings are all still choices. Once a fleet is in service …
References checked by publisher and title on 2026-11-10. Standards and regulations are cited by name only; no performance values are attributed to them. General material and logistics figures in the text are indicative reference values and should be verified against your supplier’s current data sheet and your own trial. Confirm applicability and current versions for your own operation before relying on any of them.
For a quotation, a sample box or help matching a wall thickness and closure to your loading bay and return route on site, contact service@mingplastics.com or WhatsApp +86 189 3887 1524. Include the part dimensions, the load per layer, the destination and the expected cycles per year so the recommended specification can be confirmed before you order.
For returnable packaging KPIs, Measure trips, returns and dwell time per route, and keep the calculation unchanged between reviews. The cheapest time to design an end-of-life route is before the first production order is signed.